About Industrial Screw Conveyor
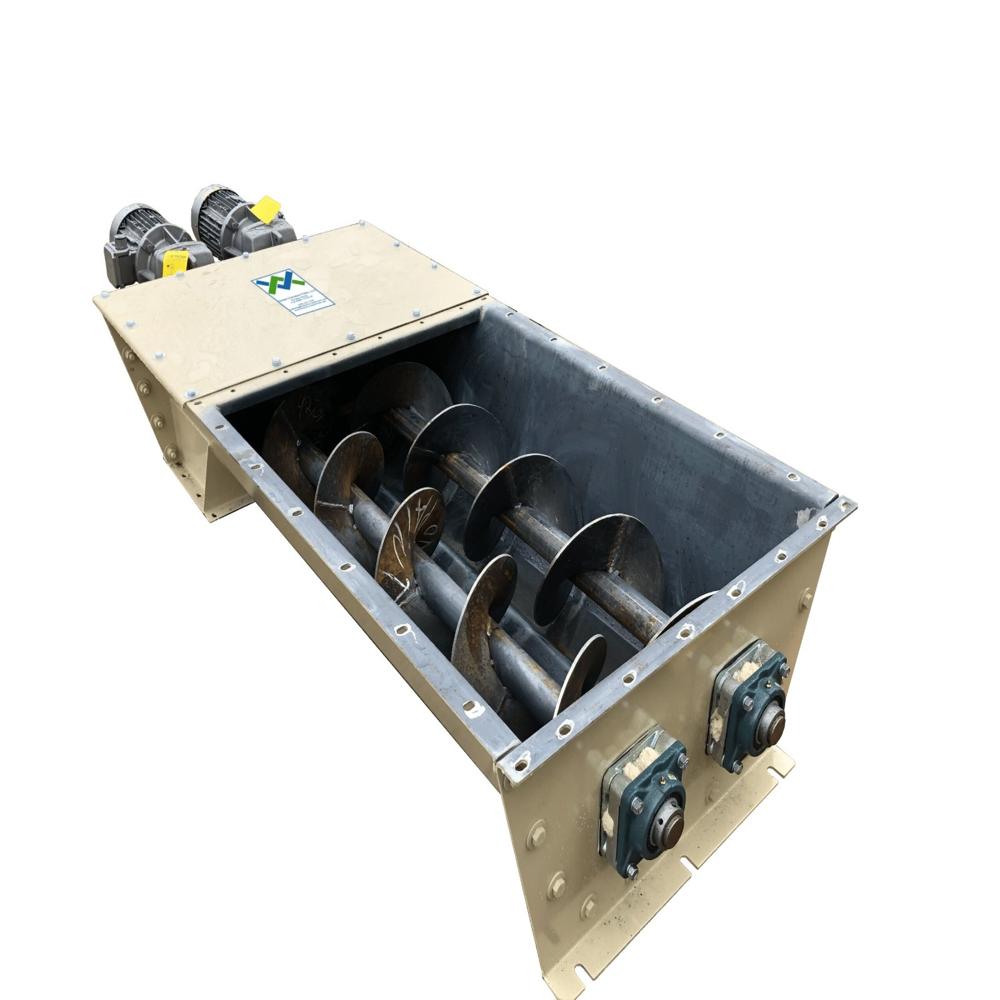
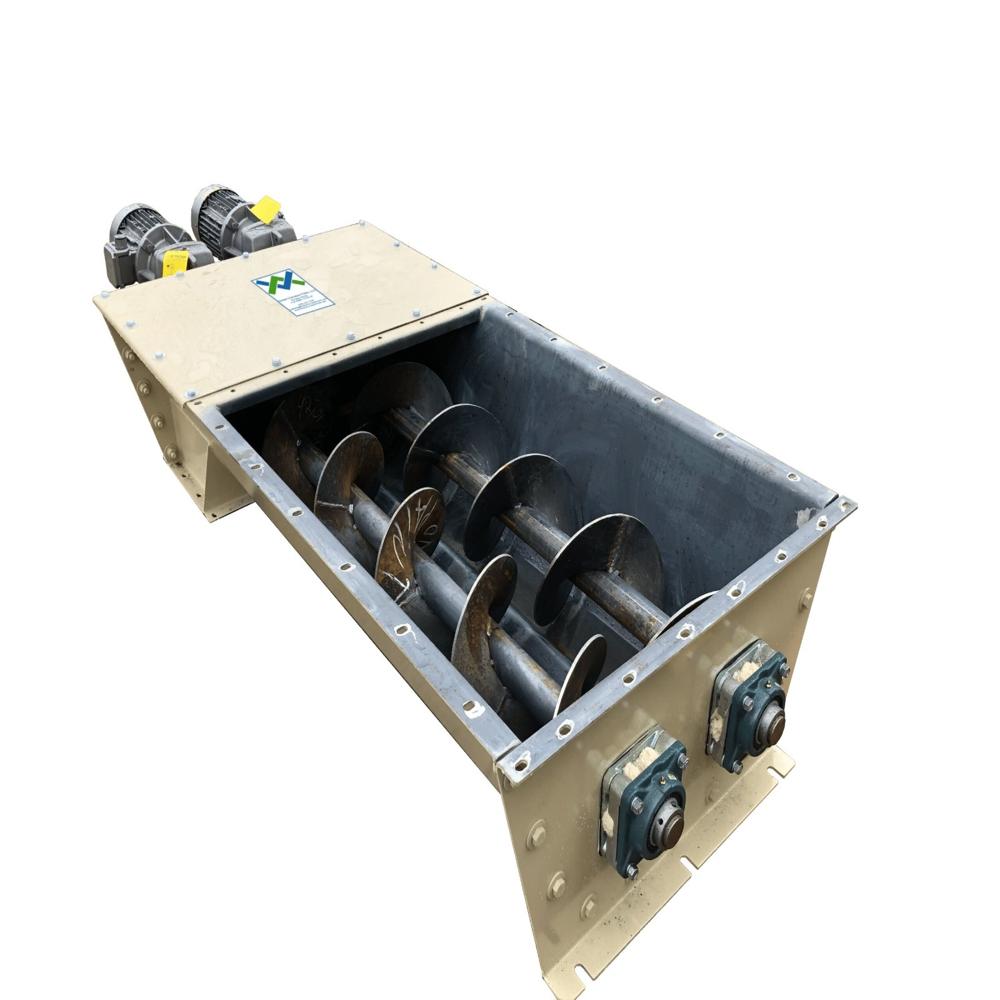
We design and manufacture Industrial Screw Conveyors for efficient and controlled handling of bulk materials in various industries. Engineered for durability and smooth operation, our screw conveyors ensure uniform material flow, minimal spillage, and reliable performance even in continuous-duty applications.
Each conveyor is custom-designed based on material characteristics, capacity requirements, and layout constraints, ensuring optimum efficiency and long service life.
Key Features
-
Robust and heavy-duty construction
-
Smooth and continuous material handling
-
Compact design requiring less floor space
-
Low maintenance and high operational reliability
-
Available in horizontal, inclined, or vertical configurations
ComponentsMaterial OptionsApplications
-
Cement and construction industry
-
Chemical and fertilizer plants
-
Food processing units
-
Power plants and PSU projects
-
Bulk material handling systems
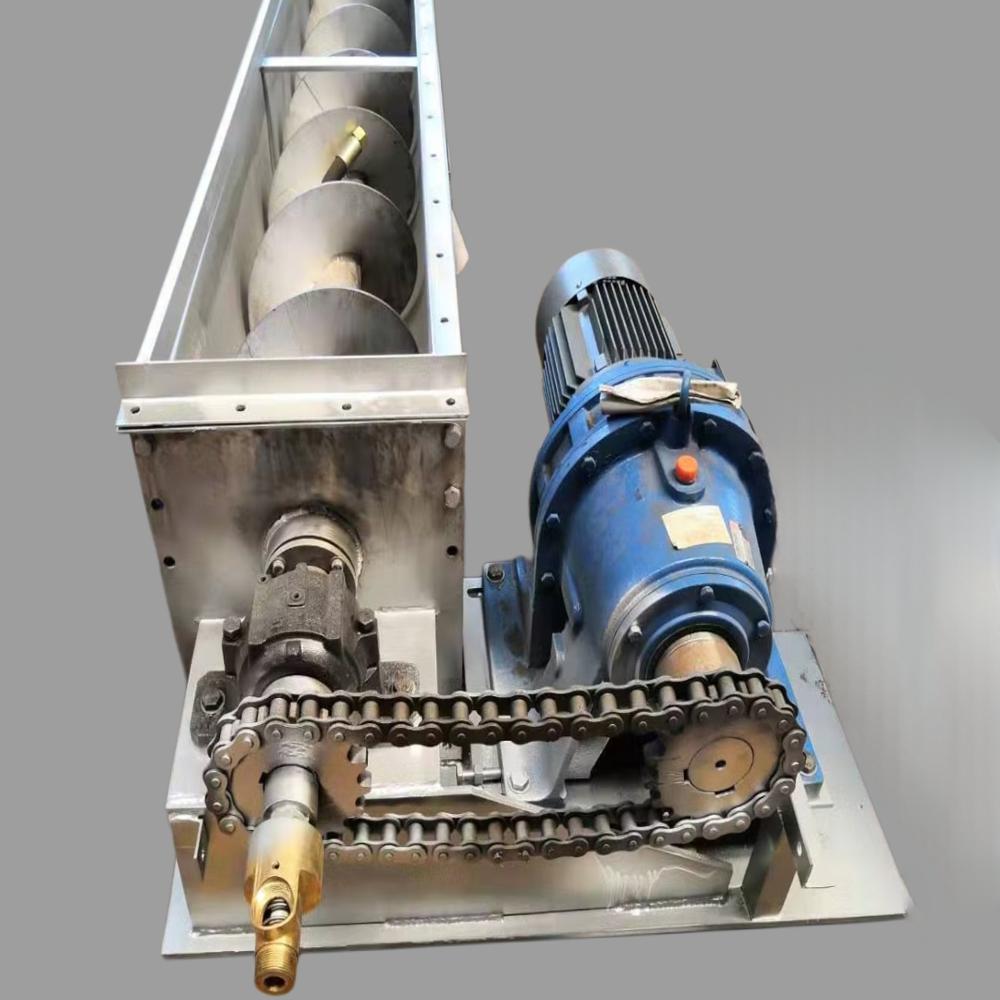
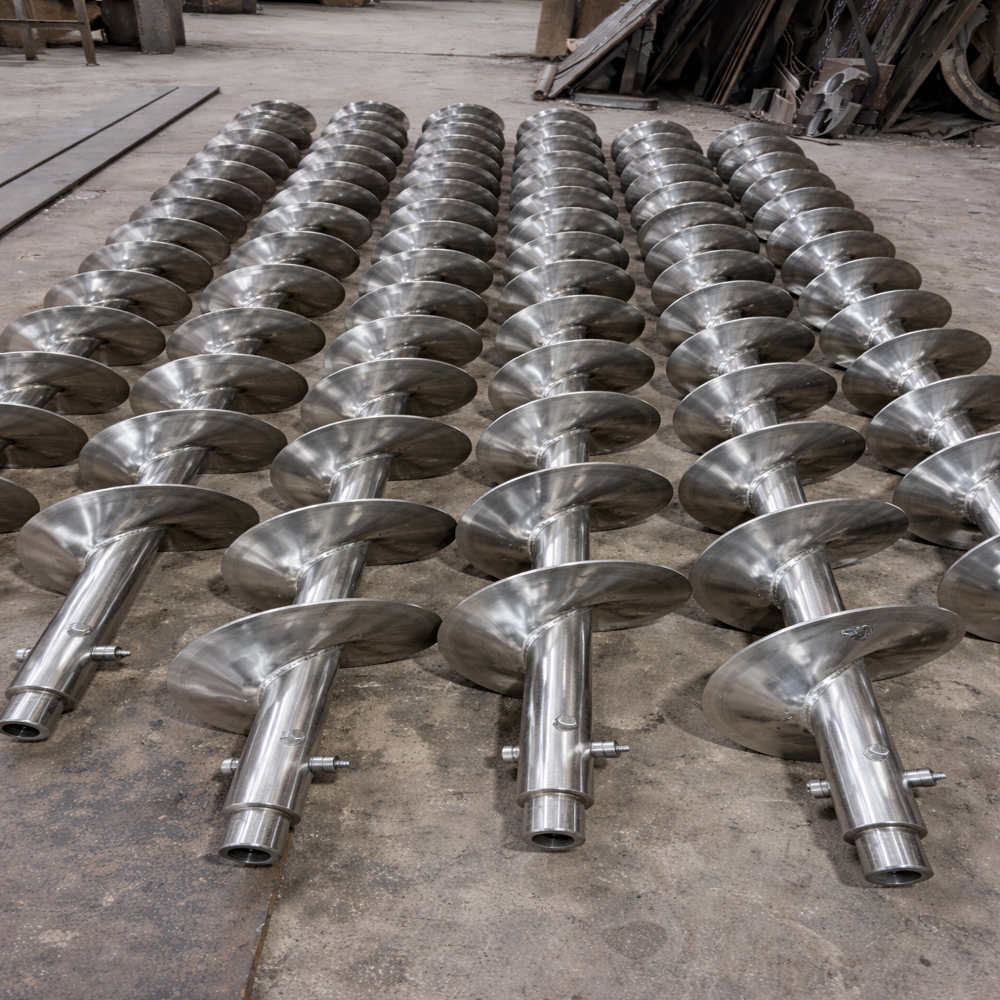
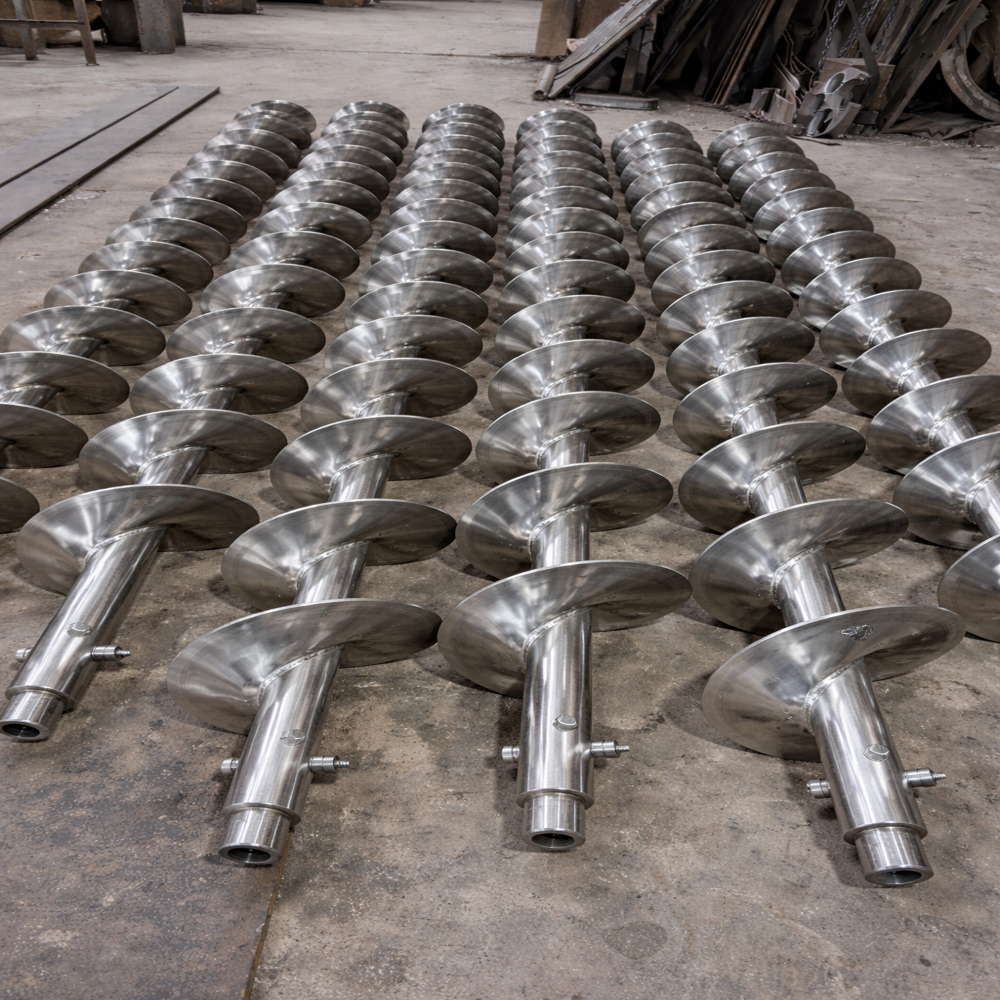
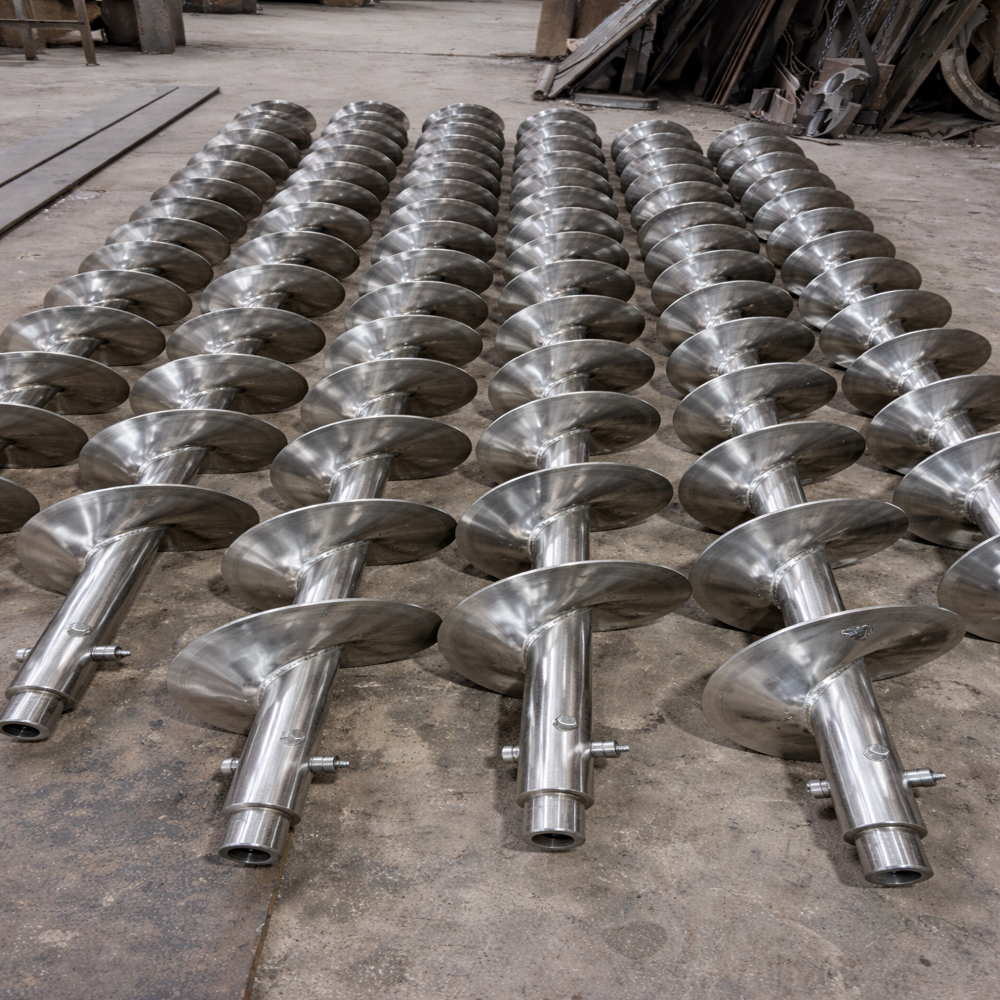
Customization & ManufacturingWe provide complete solutions from design, fabrication, machining of shafts and flights, assembly, and testing. Conveyor diameter, pitch, length, and capacity are manufactured strictly as per customer drawings and application needs.
Quality AssuranceAll screw conveyors are inspected for dimensional accuracy, alignment, and smooth rotation before dispatch to ensure reliable and long-term operation.
Customizable for Every ApplicationOur screw conveyors can be tailored for specific capacity, length, and mounting configurations. Whether you require horizontal, inclined, or vertical installation, we provide solutions to match unique process requirements, accommodating capacities from 50 kg/hr to several tons/hr and operating in temperatures up to 250C.
Robust and Reliable ConstructionChoose between stainless steel or mild steel bodies and a range of surface finishes to ensure durability and easy maintenance. With resistance to rust and corrosion, our conveyors are ideal for rigorous industrial environments, ensuring long-term reliable performance.
Flexible Operation and Easy InstallationVariable speed control up to 100 RPM, multiple discharge and inlet designs, and the availability of chain drive or gear motor drive options ensure seamless integration into your production line. Their easy installation and high efficiency further contribute to reducing downtime and optimizing productivity.
FAQ's of Industrial Screw Conveyor:
Q: How can the screw conveyor be adapted for different industrial layouts?
A: The screw conveyor offers flexible mounting options, including horizontal, inclined, and vertical installation. This allows customization to fit various plant layouts and material flow requirements, ensuring optimal integration into existing processes.
Q: What materials can be conveyed with this screw conveyor?
A: It is designed for handling a range of industrial materials such as powders, granules, and bulk solids. The conveyor is widely used in sectors like manufacturing, food processing, chemicals, and mining for efficient and dust-free transport of materials.
Q: When should I choose a vertical screw conveyor option?
A: A vertical screw conveyor is ideal when floor space is limited or when lifting materials to higher elevations is necessary. This configuration helps in space optimization and simplifies material movement in multi-level plants.
Q: Where can this conveyor be installed within a processing facility?
A: It can be installed at various points including material feed stations, intermediate transfer points, or at discharge locations. Custom-designed inlet and discharge ends ensure seamless fit to your specific equipment or hoppers.
Q: What is the process for selecting the right screw diameter and length?
A: Selection is based on your material type, required capacity, and the distance materials need to be conveyed. Our team customizes the screw diameter (100mm to 500mm) and length (up to 30 meters) to match your process needs for maximum efficiency.
Q: How does the conveyor's sealing system benefit operations?
A: Multiple sealing types, such as gland packing or mechanical seals, prevent leakage and contamination, ensuring safe and efficient handling of materials-especially those that are hazardous or dusty.
Q: What are the main benefits of using this industrial screw conveyor?
A: Key benefits include high efficiency, low noise operation, customizable design, corrosion resistance, and minimal maintenance. These features collectively enhance productivity, reduce operational downtime, and ensure safe material handling in demanding industrial environments.




 Send Inquiry


 Send Inquiry
 Send Inquiry
 Send SMS
